Skip to content

Manufacturing

The works

One roof, every process.

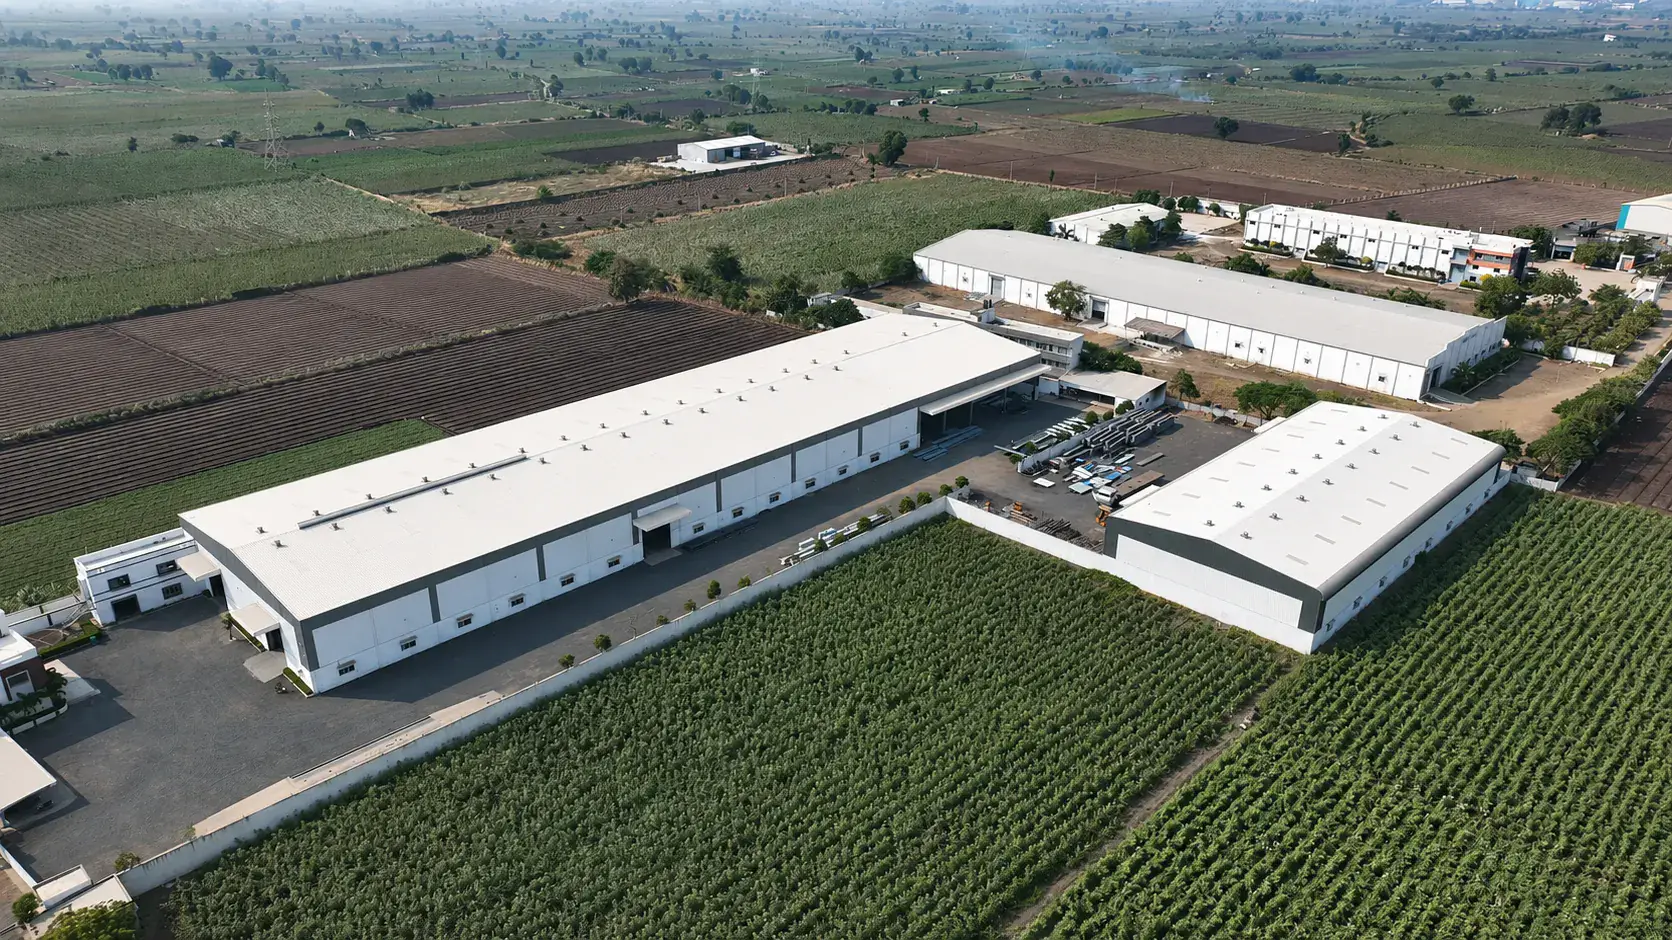
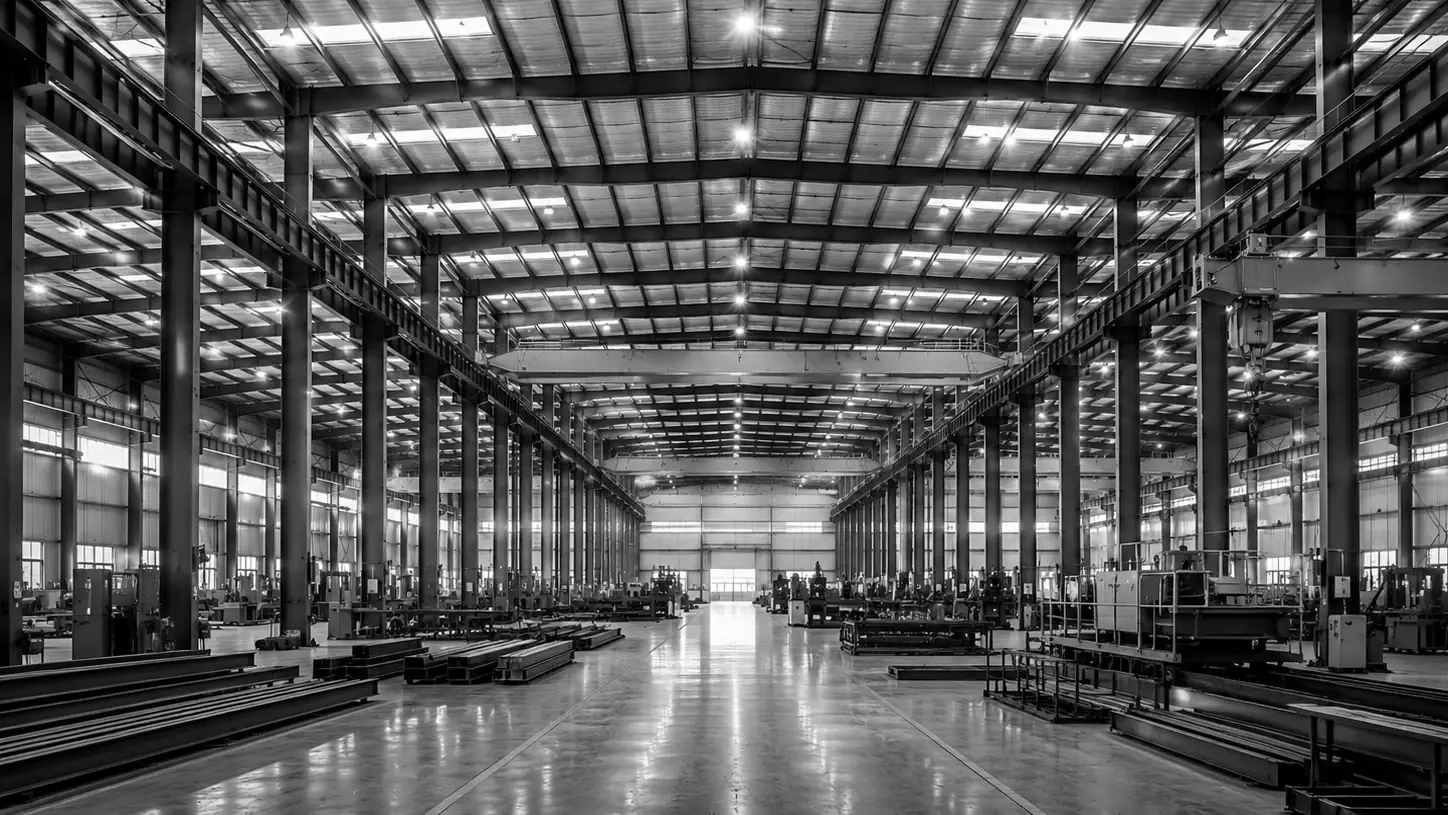
Every DSI building is made under one roof at Chhattar, on the Rajkot–Morbi highway: plate in at one end, numbered, painted members out at the other, from a 15,000 square metre works with a fully enclosed, automated production line.

Work done under a roof is work that can be measured. Plate is cut on CNC plasma and shears, built-up sections are welded on an automatic pull-through line, holes are drilled and punched to the detailing model, and every member is shot-blasted and primed before it is bundled for the erection sequence. Purlins, girts, roof and wall sheet, standing seam panels and deck sheet are roll-formed on the same floor, so the frame and its skin leave together.

The shop runs to management systems certified by TÜV SÜD for quality, environment and safety, with inspection hold points recorded against every mark number. What follows is the capacity, the certifications and the machines, one by one.

  • Annual Fabrication Capacity

    15,000MT

    Fully enclosed, automated production line

  • Manufacturing Facility

    15,000Sq. Mt.

    At Chhattar, Rajkot

  • Established

    2018

    8+ years of building

  • Projects Delivered

    230+

    Since 2018

Aerial view of the Darshan Steel Infrastructure works and yard at Rajkot, surrounded by farmland

Process

From plate to dispatch.

Nine things the shop does to every building, in the order they happen on the floor.

  1. 01

    CNC Cutting

    Profile and plate cutting to drawing geometry, with nesting to reduce offcut.

  2. 02

    CNC Drilling

    Hole positions driven from the detailing model so bolt groups line up at assembly.

  3. 03

    Automatic Welding

    Submerged-arc welding of built-up sections for consistent, repeatable weld profiles.

  4. 04

    Built-Up Section Fabrication

    Tapered I-sections assembled from plate so depth follows the bending moment diagram.

  5. 05

    Surface Preparation

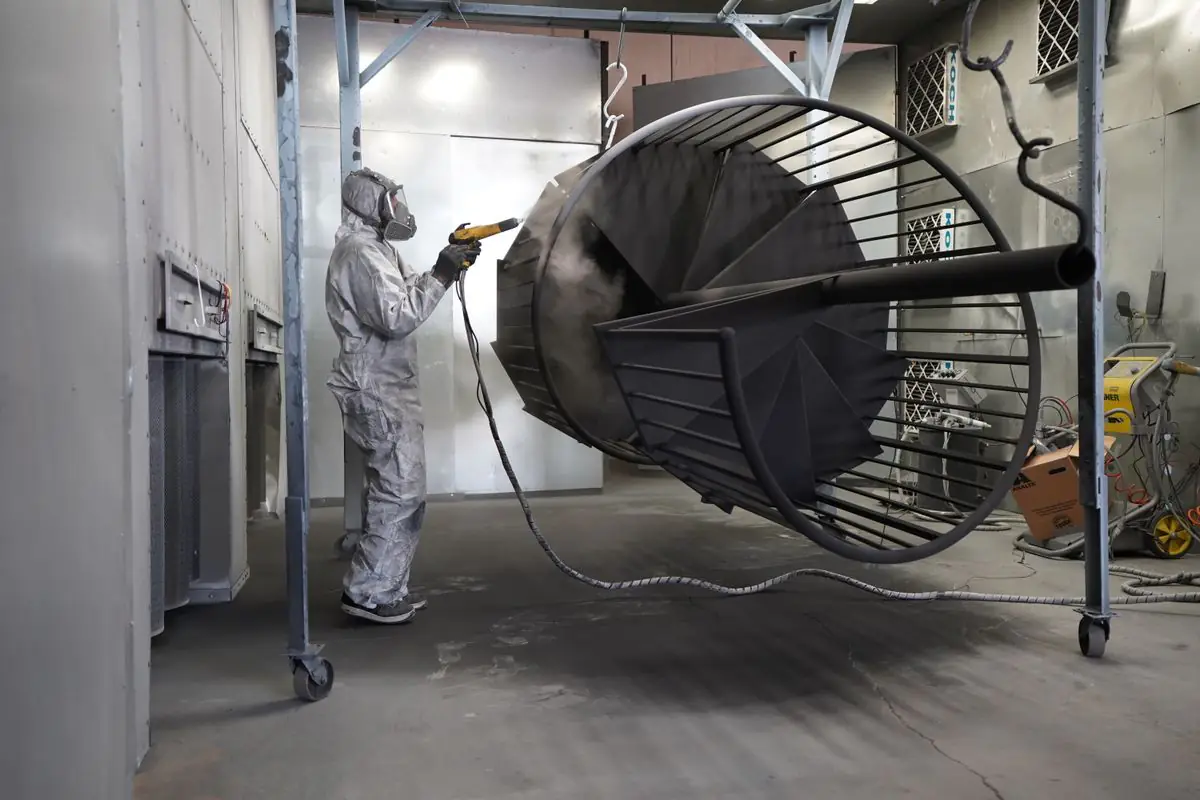
    Blast cleaning to the specified surface profile before any coating is applied.

  6. 06

    Coating & Painting

    Primer and finish systems selected for the operating environment, with film thickness recorded.

  7. 07

    Quality Inspection

    Dimensional and weld inspection at fixed hold points, documented against each mark.

  8. 08

    Material Handling

    Crane-served bays and staging areas that keep members moving through the shop in sequence.

  9. 09

    Dispatch Management

    Bundling and loading planned around the erection sequence, not around truck convenience.

Certifications

Three systems, certified by TÜV SÜD.

Quality, environment and safety, each run as a management system that is audited by an independent body. The certificates themselves are below.

Certified scope
Manufacturing and supply of pre-engineered building and fabricated steel structure
Validity
to Subject to successful completion of annual periodic audits
Certification body
TÜV SÜD South Asia Private Limited
  • ISO 9001:2015

    Quality management system

    Certified by TÜV SÜD
    ISO 9001:2015 certification mark, TÜV SÜD

    The international standard for a quality management system: a documented way of working that starts from what the customer needs, controls every process that delivers it, checks the result, and corrects the process when something goes wrong.

    What the standard requires

    • Documented procedures from enquiry to handover, with responsibilities fixed
    • Control of design, purchasing, production and inspection as defined processes
    • Traceability of material and records against each order
    • Internal audits, management review and corrective action
    • Measurement of customer satisfaction and continual improvement

    How it works on the DSI floor

    • Incoming plate and sections are checked against mill certificates and the material schedule
    • Six inspection hold points on every member: material, dimensions, welds, blast profile, coating thickness and final release
    • Measuring instruments are calibrated and records are kept by mark number
    • Non-conformances are recorded, contained and closed with a corrective action
  • ISO 14001:2015

    Environmental management system

    Certified by TÜV SÜD
    ISO 14001:2015 certification mark, TÜV SÜD

    The standard for managing the environmental impact of an operation: identifying where the work touches air, water, land and resources, meeting the law that applies, setting objectives to do better, and proving it with records.

    What the standard requires

    • Identification of environmental aspects and their impacts
    • Compliance with applicable environmental law and permits
    • Objectives, controls and monitoring for waste, emissions and resource use
    • Emergency preparedness for spills and releases
    • Audits, management review and continual improvement

    How it works on the DSI floor

    • Plate is nested on the CNC cutter to cut offcut, and steel scrap is segregated and recycled
    • Abrasive is reclaimed inside the enclosed shot-blast machine rather than blown into the yard
    • Paints, solvents and their containers are stored, used and disposed of under control
    • Energy and water use are monitored against targets
  • ISO 45001:2018

    Occupational health and safety management system

    Certified by TÜV SÜD
    ISO 45001:2018 certification mark, TÜV SÜD

    The standard for keeping people safe at work: finding the hazards in every task, reducing the risk before the work starts, involving the workers themselves, and learning from every incident and near miss.

    What the standard requires

    • Hazard identification and risk assessment for every activity
    • Worker consultation and participation in safety decisions
    • Operational controls, permits and emergency plans
    • Training and competence for the task in hand
    • Incident investigation, audits and continual improvement

    How it works on the DSI floor

    • PPE is standard in the shop and on site: helmets, eye protection, harnesses at height and safety footwear
    • Lifting plans, exclusion zones and temporary bracing are agreed before a member leaves the ground
    • Machine guarding, hot-work control and fume and dust management on the cutting, welding and blasting lines
    • Every crew is briefed on the method statement for the work in front of it

Six hold points on every member

The quality system in practice: a member does not move to the next stage until the check for the last one is recorded against its mark number.

  1. 01

    Material Inspection

    Incoming plate and sections checked against mill documentation and the material schedule.

  2. 02

    Dimensional Accuracy

    Member length, depth, camber and hole position verified against the shop drawing.

  3. 03

    Welding Quality

    Weld size, profile and continuity inspected; procedures and welders qualified to the project specification.

  4. 04

    Surface Preparation

    Blast profile and cleanliness confirmed before coating is applied.

  5. 05

    Coating Inspection

    Dry film thickness measured and recorded across each coated member.

  6. 06

    Final Quality Check

    Fit-up, marking and completeness verified against the packing list before release.

Plant & machinery

Machines on the floor.

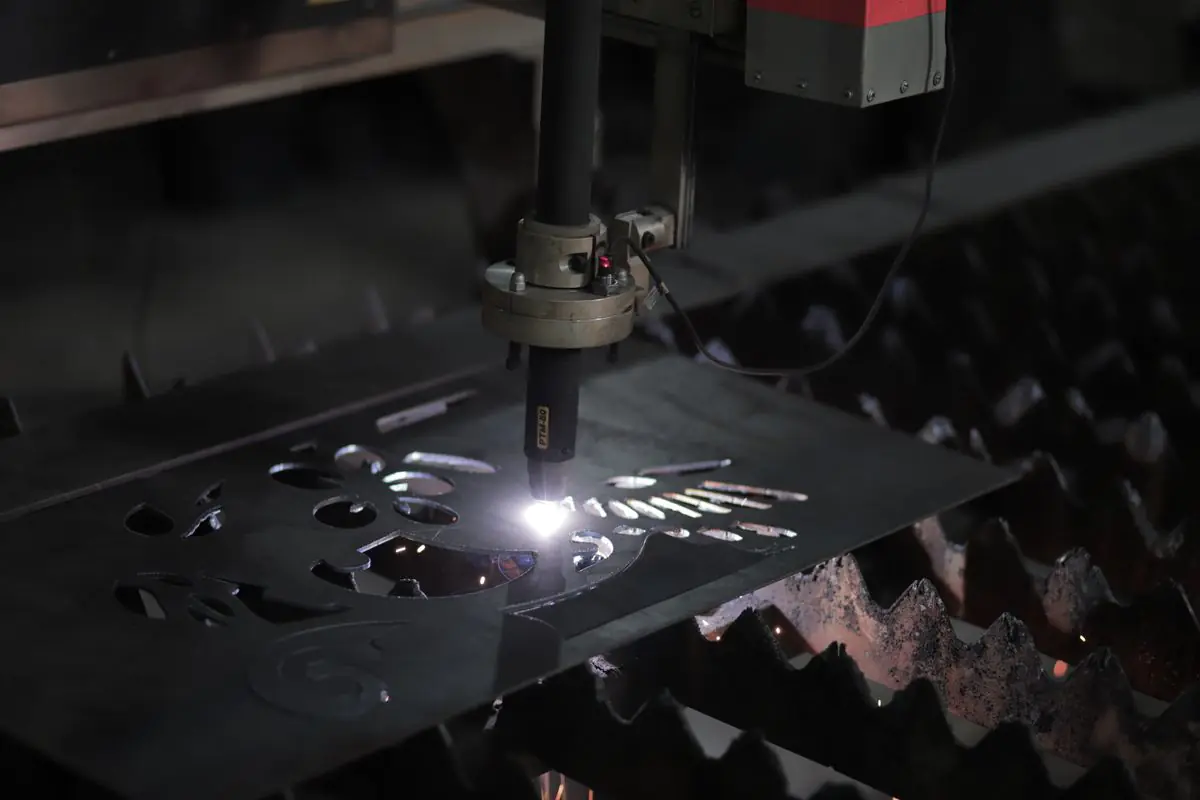
  • CNC plasma torch cutting a shape from steel plate, the arc lighting the cut

    Cutting & shearing

    CNC Plasma Cutting Machine

    Cuts webs, flanges, stiffeners and gusset plates from plate to the nested CNC programme.
    Operation
    Automatic, CNC
    Cutting thickness
    20 mm recommended, 32 mm piercing
    Bed size
    4,000 mm × 15,500 mm
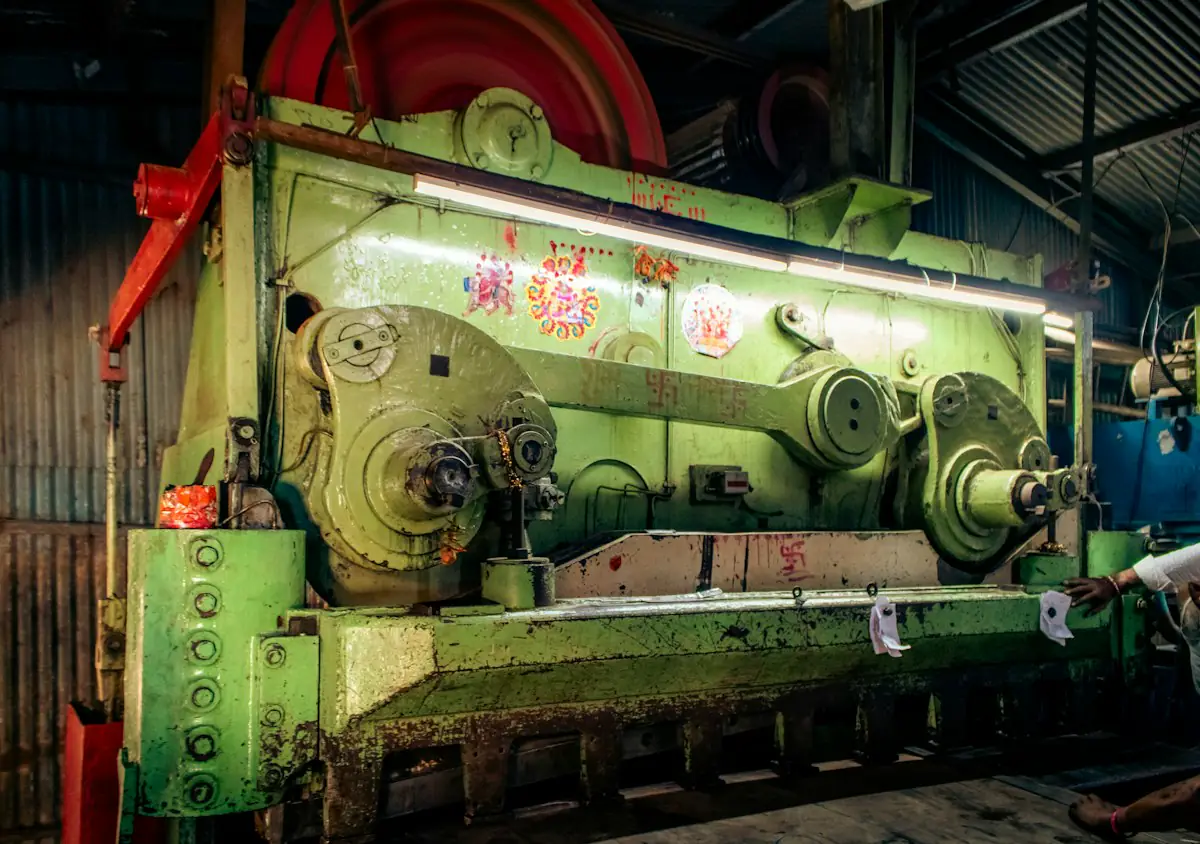
  • A large green guillotine shearing machine in a fabrication shop

    Cutting & shearing

    CNC Shearing Machine

    Straight cuts in plate and sheet to programmed length, for flange strips, cleats and flashings.
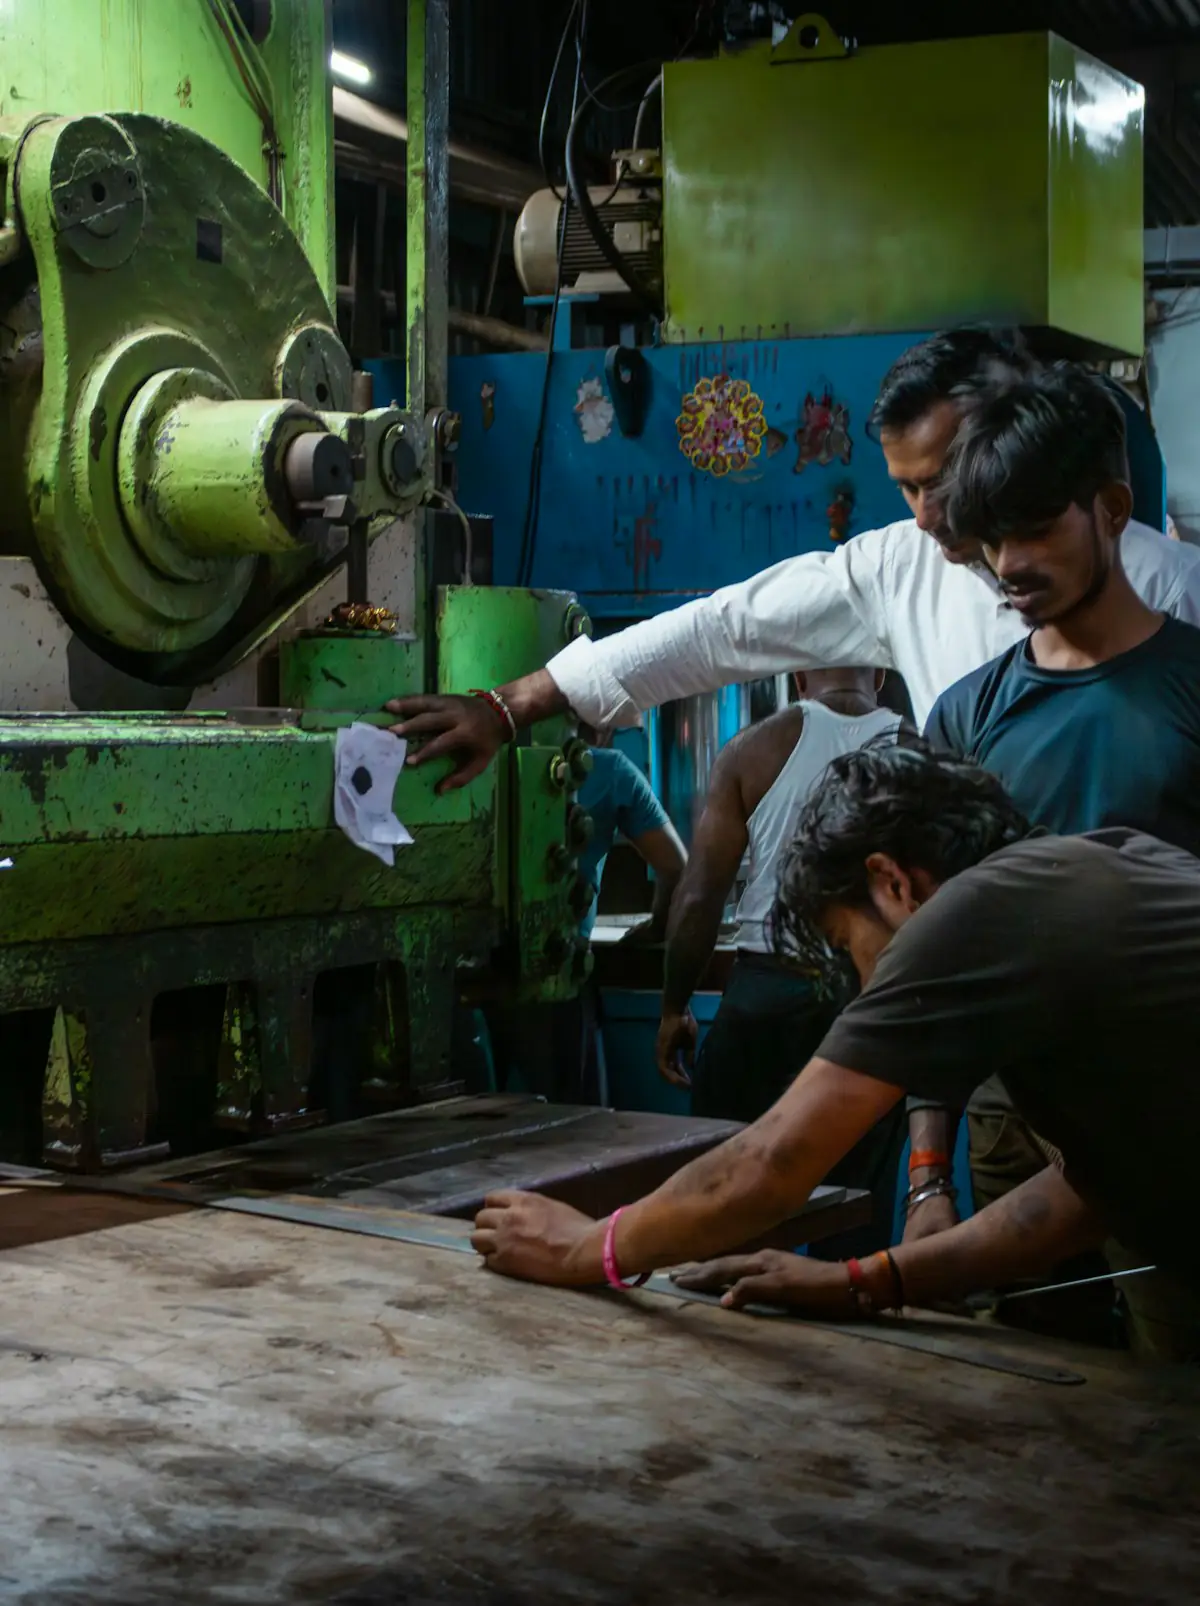
    Operation
    Automatic, CNC
    Cutting length
    6 m
    Thickness
    Up to 20 mm
  • Operators feeding a steel sheet into a guillotine shearing machine
    3 units

    Cutting & shearing

    Shearing Machines

    Three semi-automatic shears for lighter plate, sheet and trim, sized so the CNC shear is kept for heavy work.

    Operation
    Semi-automatic
    Cutting lengths
    3 m, 3 m and 1 m
    Thickness
    14 mm, 4 mm and 12 mm

    3 units on the floor

    • 3 m × 14 mm
    • 3 m × 4 mm
    • 1 m × 12 mm
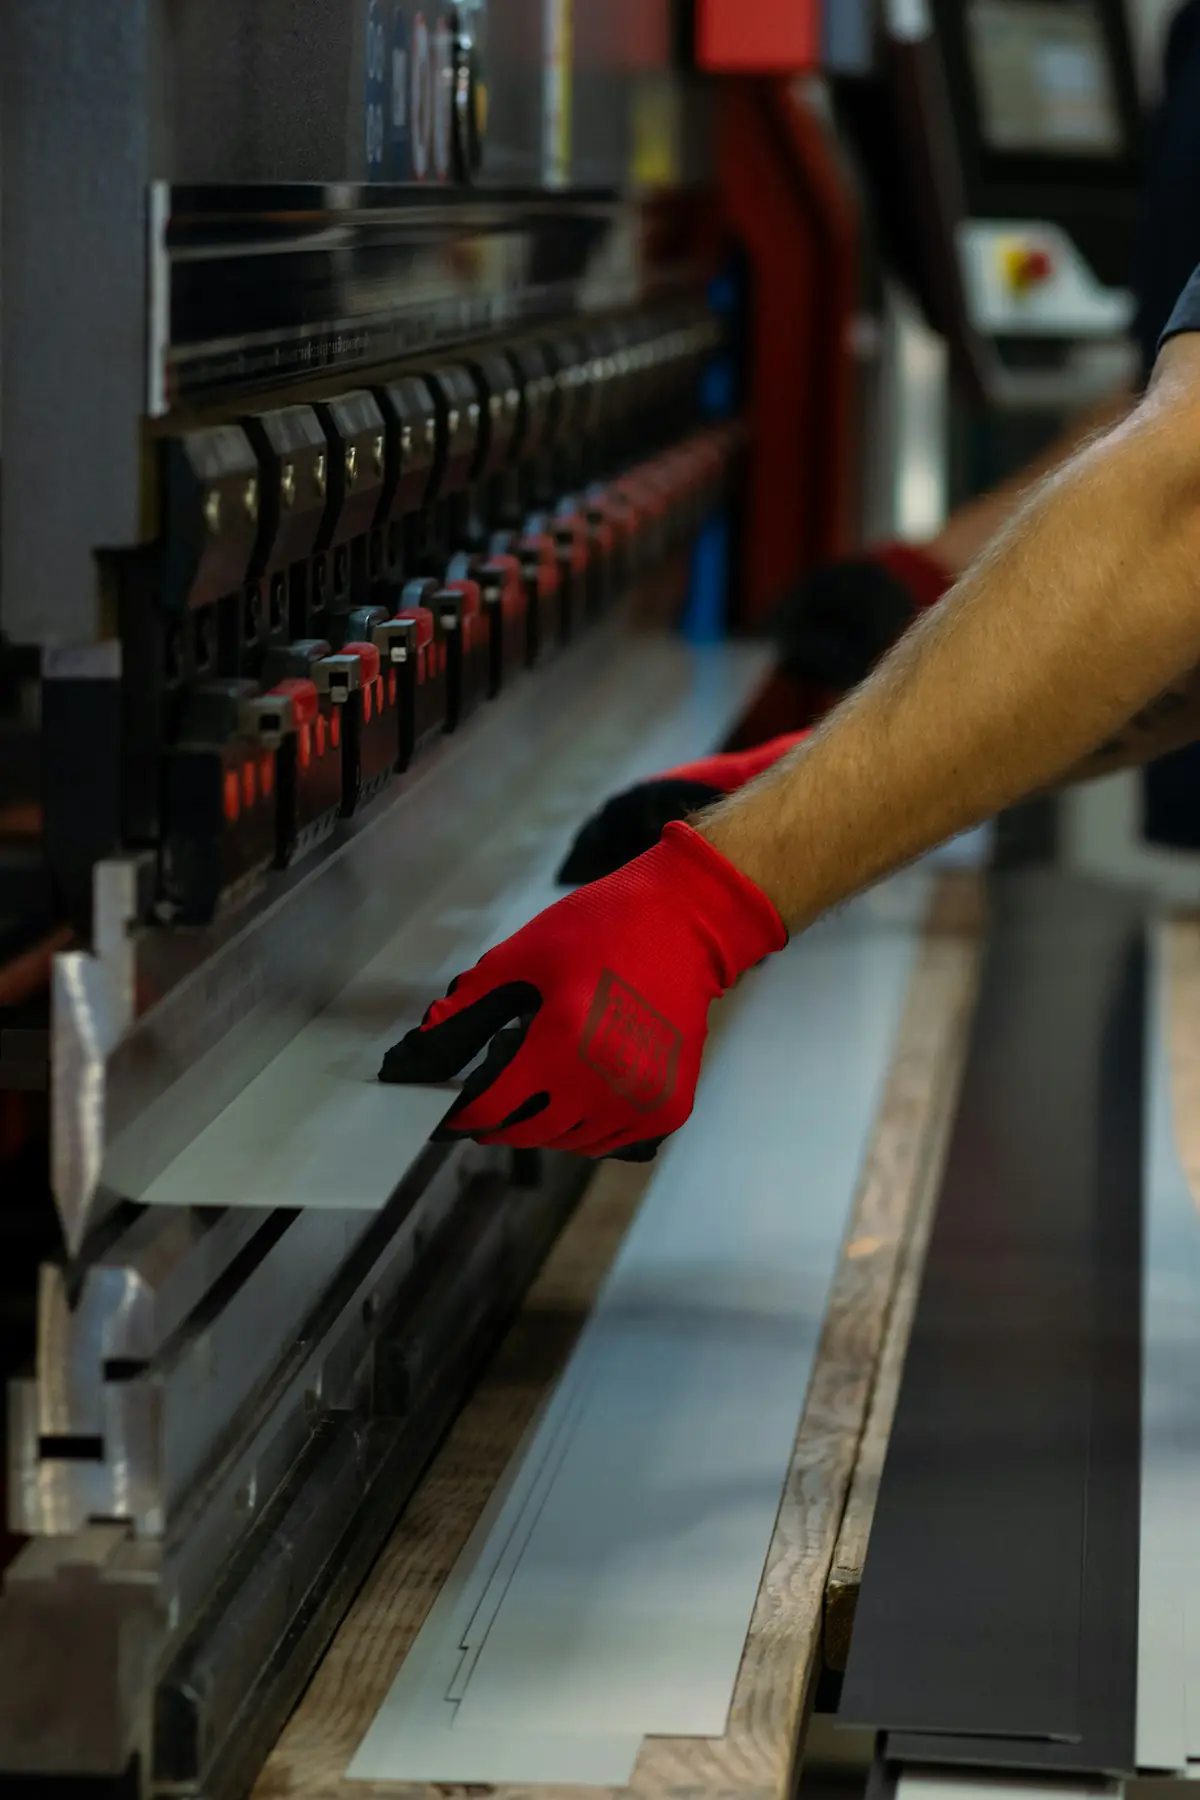
  • A gloved hand positioning sheet under the tooling of a CNC press brake

    Bending & pressing

    CNC Press Brake

    Bends sheet into flashings, trims, closures, gutters and brackets to the programmed angle.
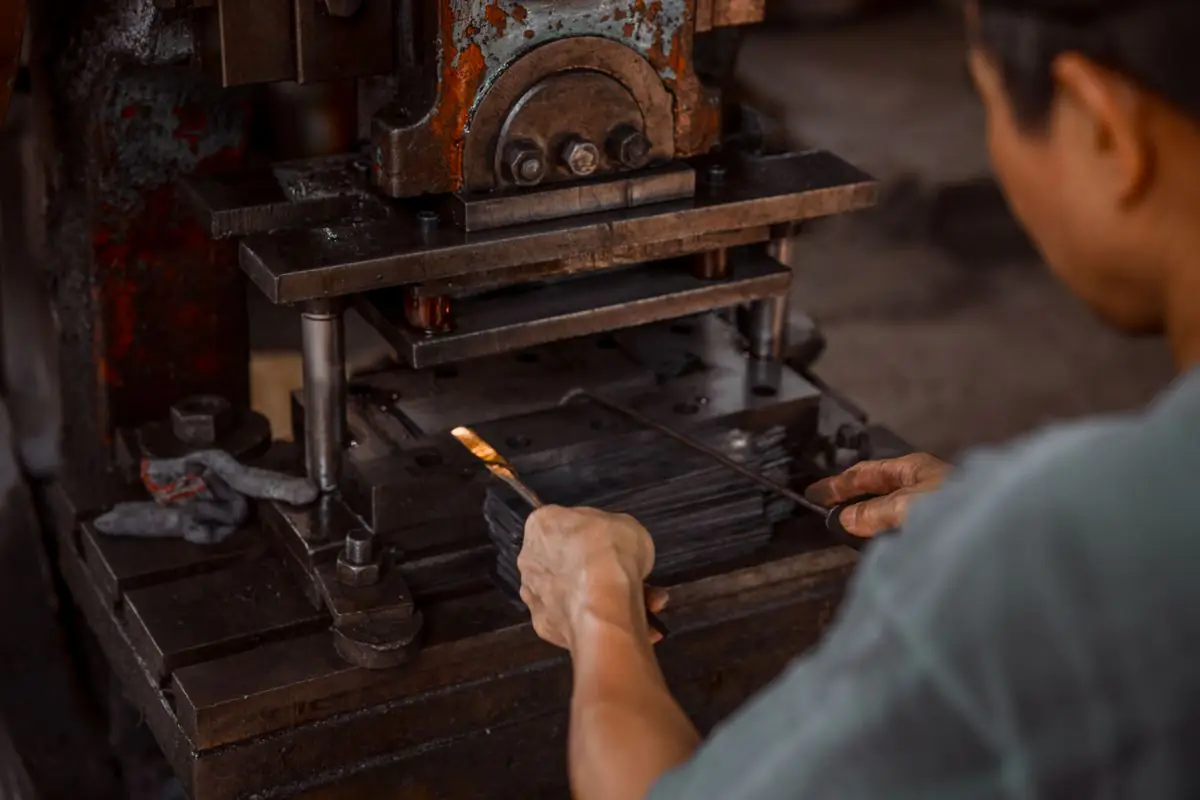
    Operation
    Automatic, CNC
    Capacity
    80 tonnes
    Sheet thickness
    0.5 mm to 3 mm
  • An operator feeding a strip into a mechanical power press

    Bending & pressing

    Mechanical Power Press

    Presses and blanks small fittings, cleats and washers in volume.
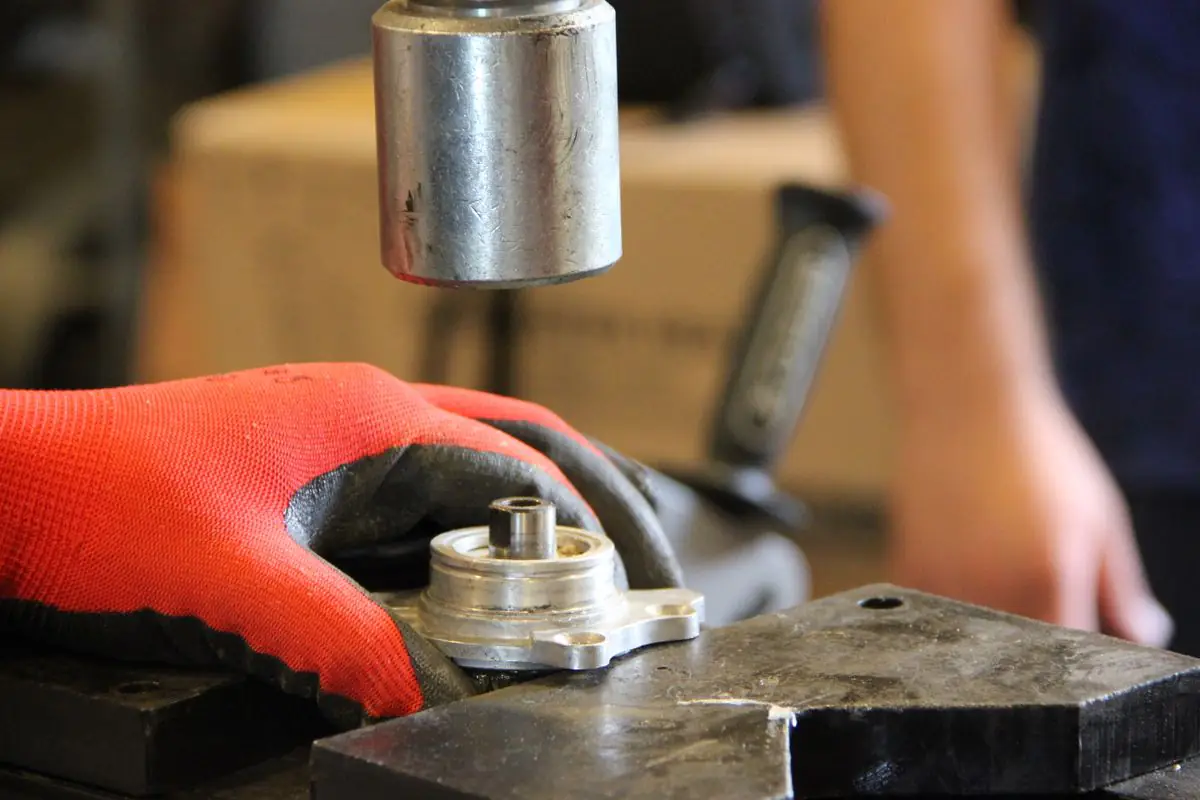
    Operation
    Manual
    Capacity
    150 tonnes
  • A hydraulic ram pressing a steel component on a punching bed
    3 units

    Drilling, punching & threading

    Hydraulic Punching Machines

    Punches bolt holes and slots in cleats, plates and cold-formed sections faster than drilling.

    Operation
    Semi-automatic
    Capacities
    240, 100 and 60 tonnes
    Tooling
    Single punch, four-punch and slot

    3 units on the floor

    • Punch hole, 240 tonnes
    • Four-punch hole, 60 tonnes
    • Slot hole, 100 tonnes
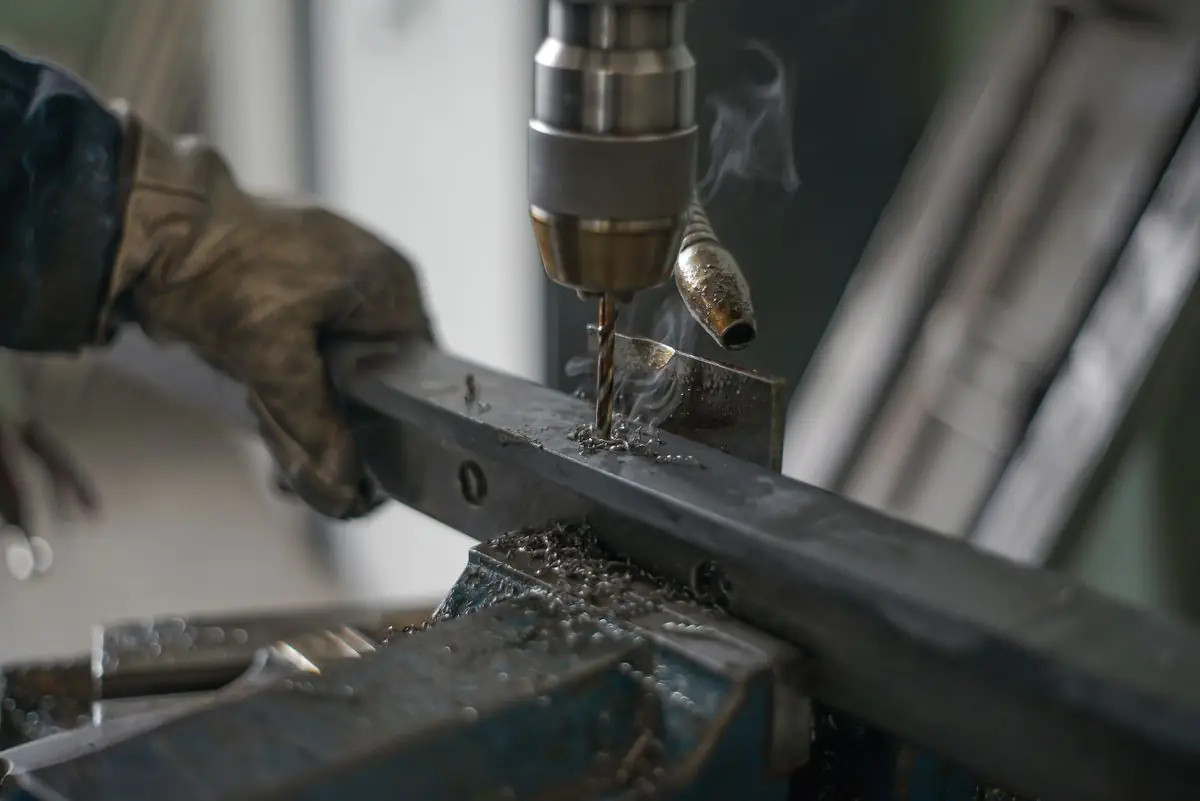
  • A drill boring a bolt hole in a steel bar, swarf curling from the bit
    2 units

    Drilling, punching & threading

    Radial Drill Machines

    Drills bolt holes in end plates, base plates and flanges where punching is not suitable.

    Operation
    Semi-automatic
    Hole diameter
    Up to 50 mm
    Bed and reach
    1 m × 1 m bed, 1 mm to 600 mm thickness

    2 units on the floor

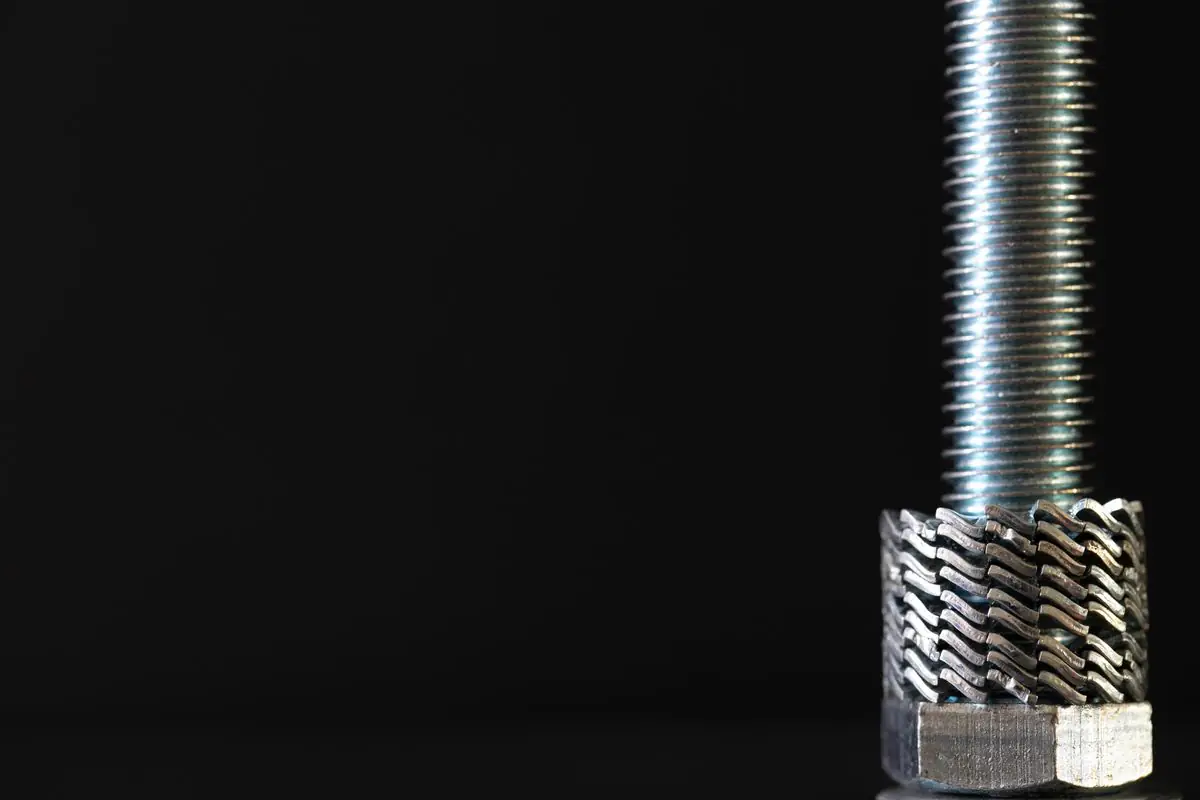
  • Close-up of a rolled thread on a steel rod

    Drilling, punching & threading

    Hydraulic Thread Rolling Machine

    Rolls threads on sag rods, bracing rods and anchor bolts, which are stronger than cut threads.
    Operation
    Semi-automatic
    Rod diameter
    10 mm to 12 mm
  • Automatic welding heads running along a large steel section on a welding line

    Welding

    PHI Pull-Through Automatic Welding Line

    Welds web to flanges on built-up tapered sections in one continuous pass, both sides at once.
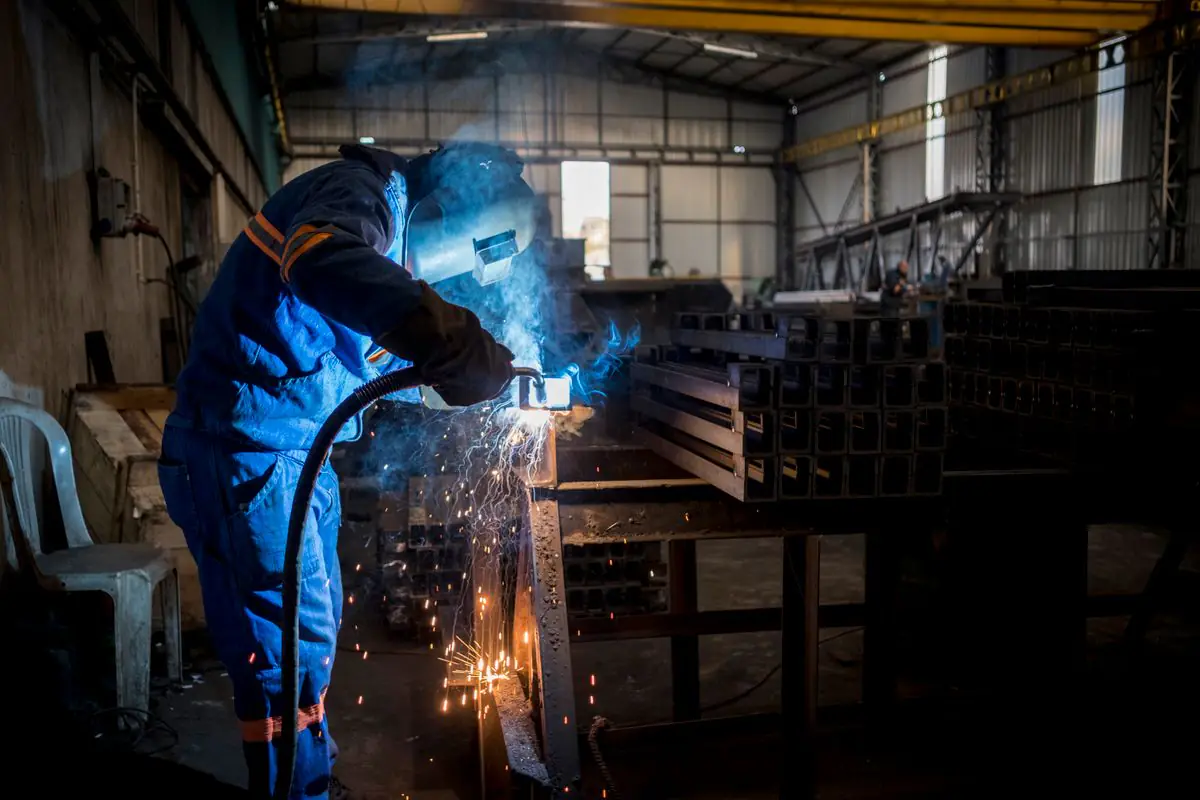
    Operation
    Semi-automatic
    Travel speed
    0.5 to 1.8 m/min
    Welding power
    90 kVA
  • A welder MIG welding steel sections inside a fabrication shop
    13 units

    Welding

    MIG Welding Sets

    Fit-up, stiffeners, end plates, cleats and every weld the automatic line does not reach.

    Operation
    Manual, three-phase
    Rating
    10 kVA
    Travel speed
    Up to about 1 m/min

    13 units on the floor

  • An operator in a hooded suit treating a large steel component inside an enclosed booth

    Surface preparation

    Shot Blasting Machine

    Blasts every member to the specified surface profile before the primer goes on.
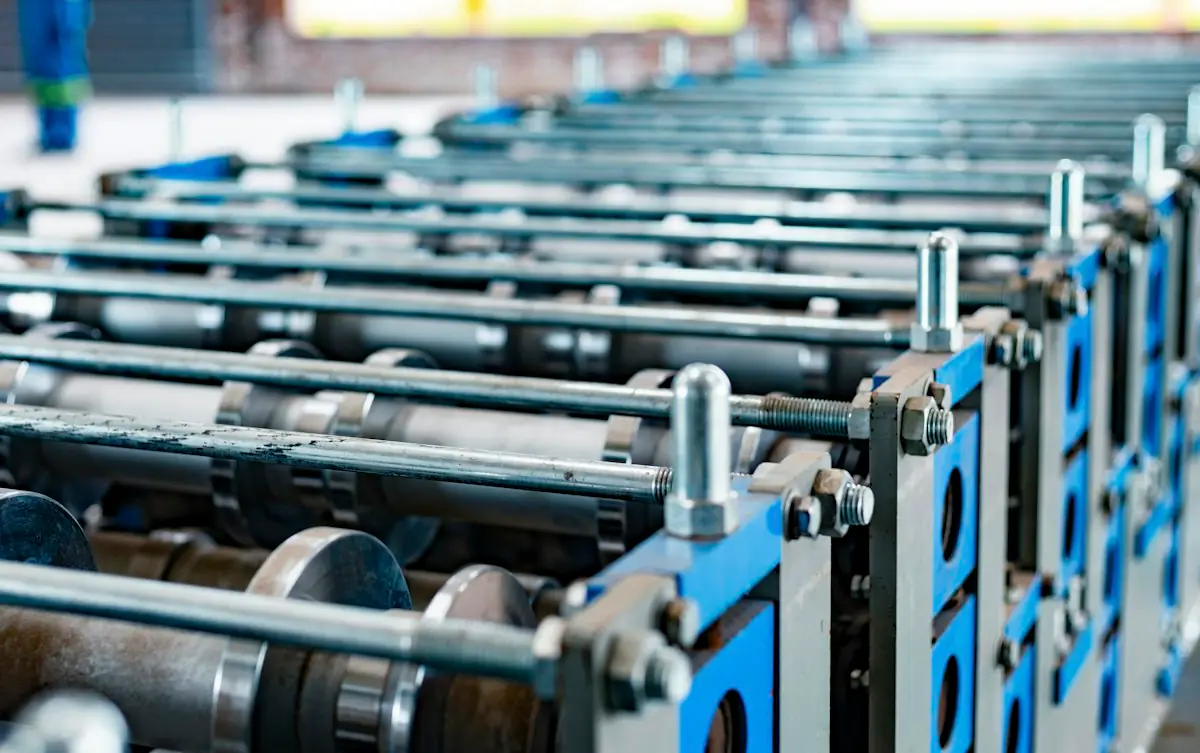
    Operation
    Automatic
    Conveyor speed
    0.5 to 5 m/min
    Abrasive throughput
    2,400 to 4,000 lb/min
    Air volume
    18,000 m³/h
  • The roller stands of a cold roll-forming line for purlins and girts

    Roll forming

    C/Z Purlin Roll Forming Machine

    Forms the cold-formed Z and C purlins and girts that span between the frames.
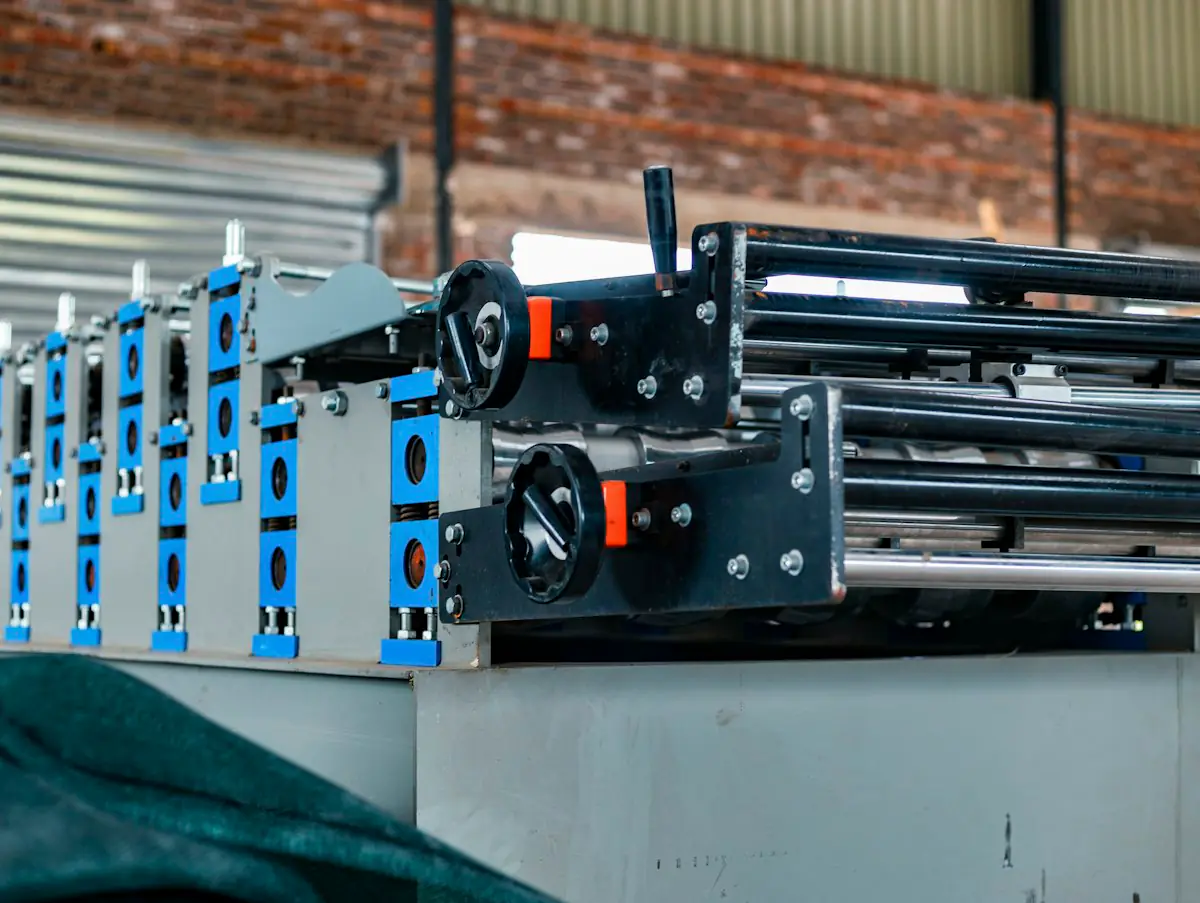
    Operation
    Automatic
    Material thickness
    Up to 2.5 mm
  • A sheet roll-forming machine with blue roller stands in a workshop

    Roll forming

    Roof & Wall Sheet Forming Machine

    Roll-forms the trapezoidal roof and wall sheet from coil, in single lengths to order.
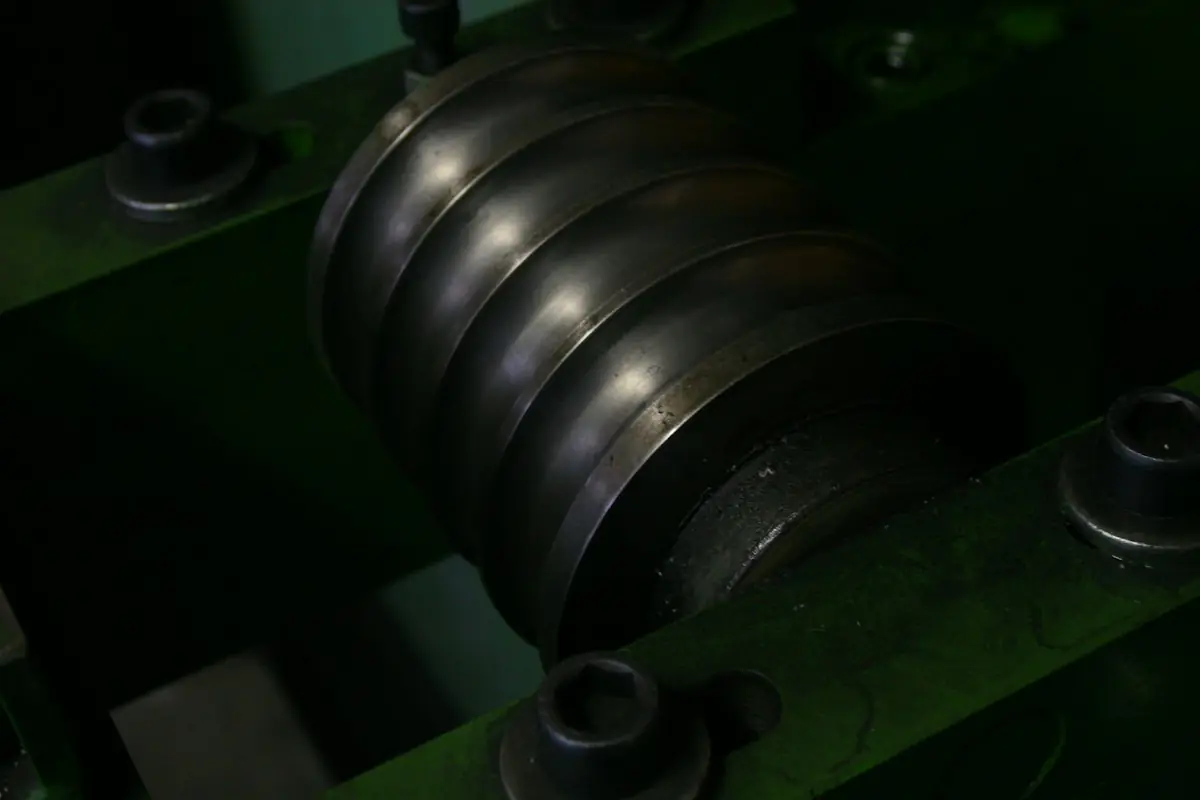
    Operation
    Automatic
    Sheet thickness
    0.6 mm
  • Close-up of a grooved forming roller on a roll-forming machine

    Roll forming

    Standing Seam Roll Forming Machine

    Forms the clip-fixed standing seam roof panel with no fastener through the sheet.
    Operation
    Automatic
    Sheet thickness
    0.6 mm
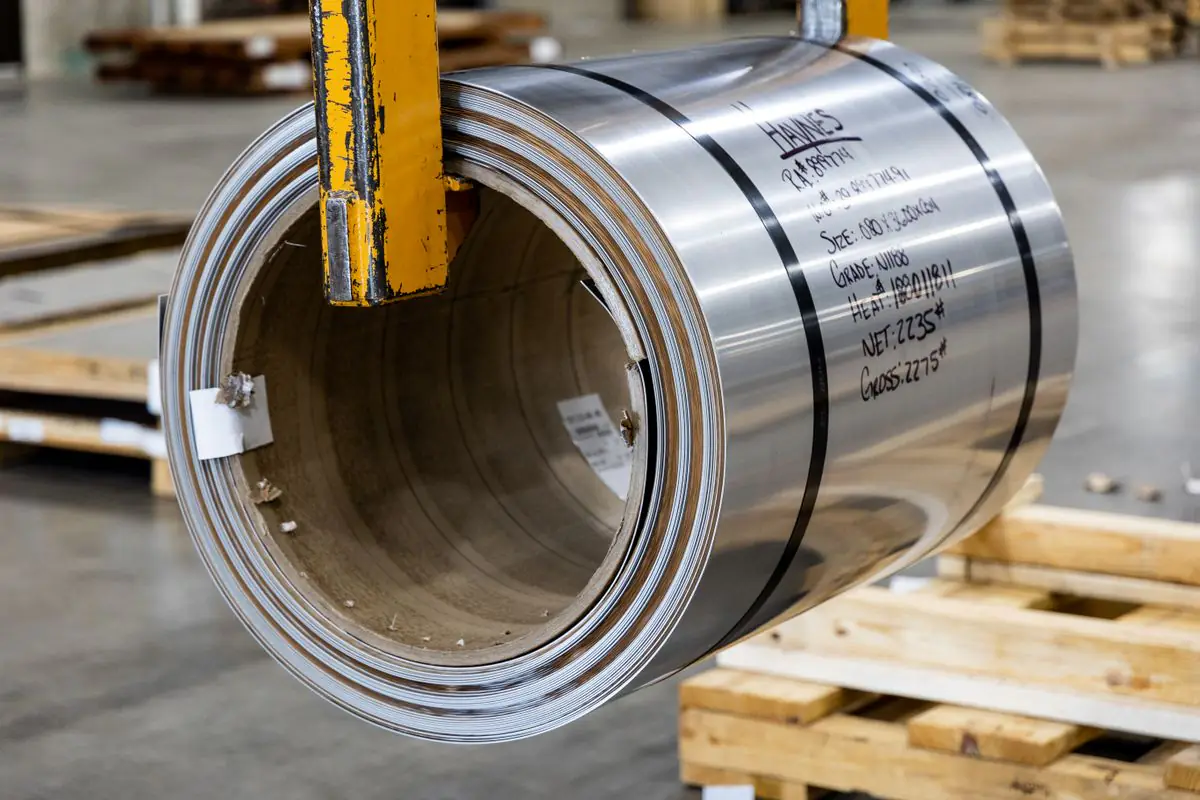
  • A steel coil on a crane hook, ready to feed a forming line

    Roll forming

    Deck Sheet Forming Machine

    Forms the profiled deck sheet that carries the concrete slab on a mezzanine floor.

    Operation
    Automatic
    Sheet thickness
    1.6 mm

Next step

See the works for yourself.

Clients and consultants are welcome at Chhattar to walk the floor and see their steel being made. Ask for a visit, or send us the building and we will send you the programme.

Survey No. 169/P4/P1, At, Rajkot - Morbi Hwy, Chhattar, Gujarat 363650